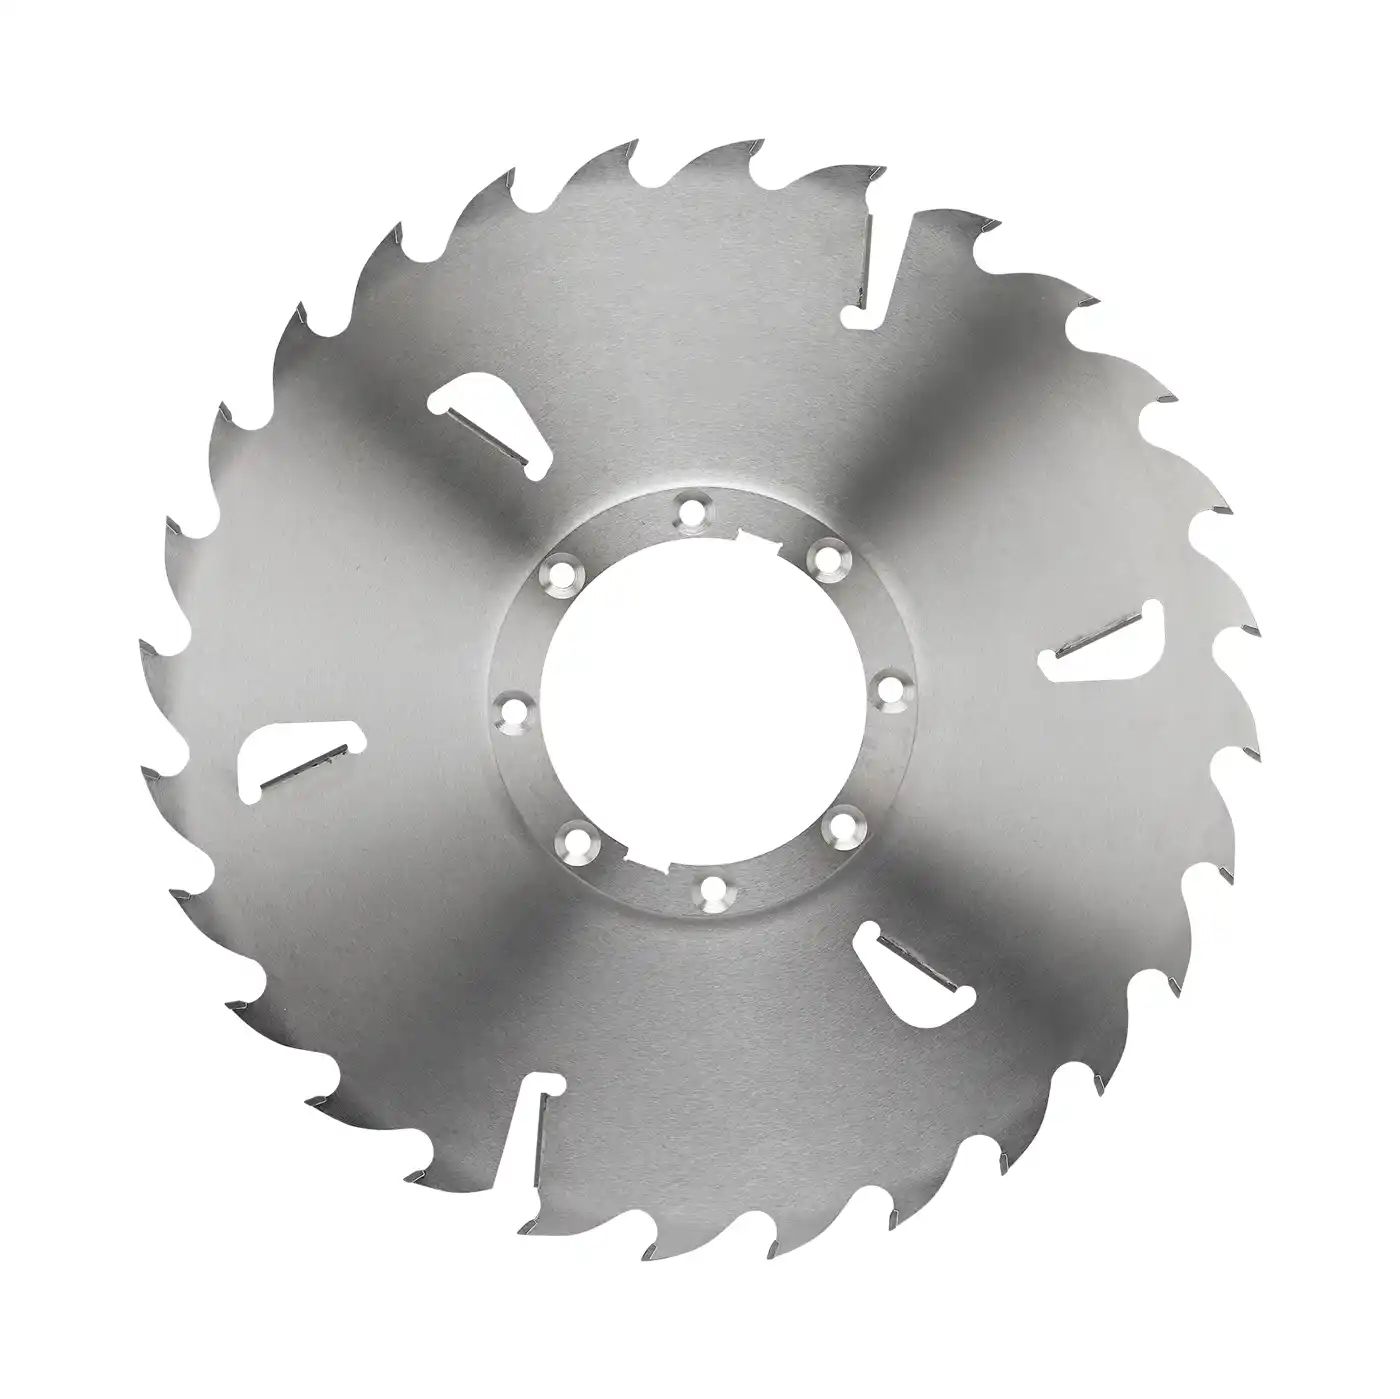
Typical Applications
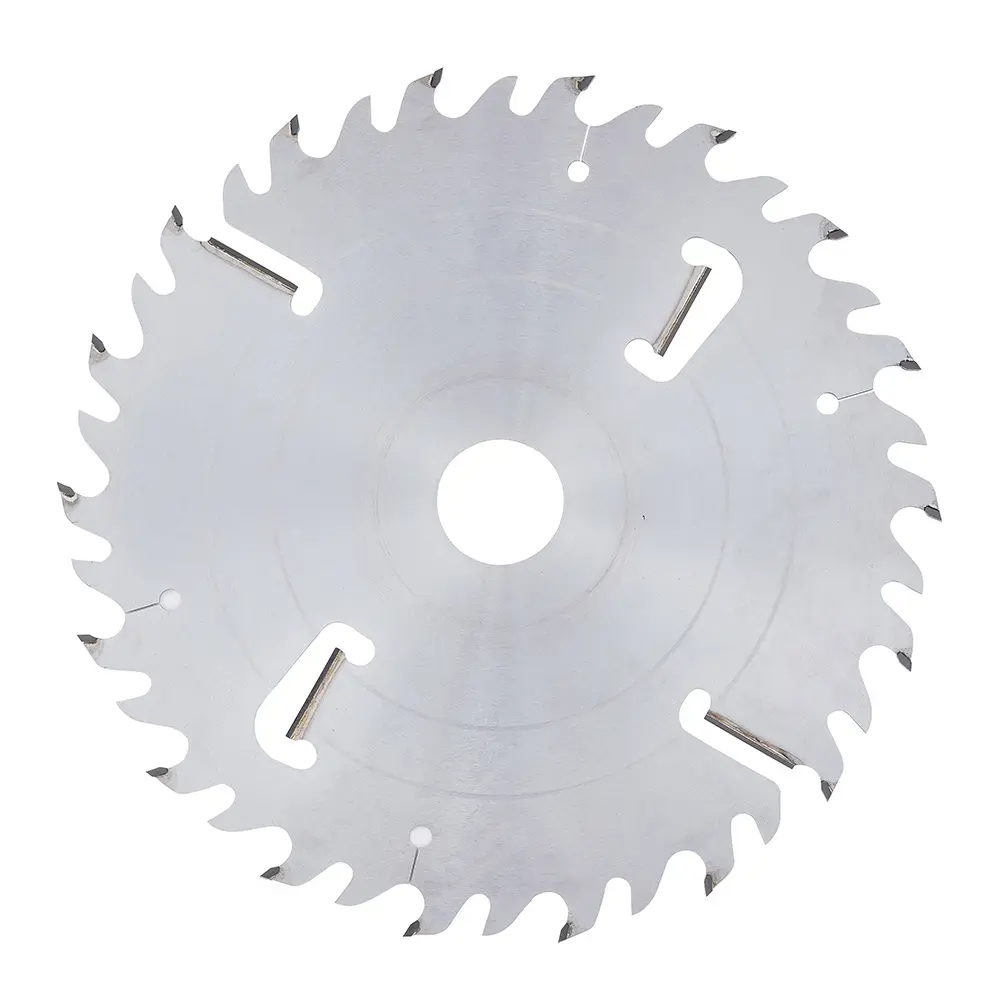
- Primary sawmill gang rip lines in softwood and hardwood sawmill plants, running wet or dry timber (spruce, pine, fir, and others).
- Multi-rip machines with and without chippers — Linck, EWD, Möhringer, SAB, Brodbaek, and equivalent.
- Automated, high-volume longitudinal ripping where stable running across a full blade set is critical.
- Dimension lumber production requiring consistent strip width and clean side faces.
Key Performance Advantages
- Thickened convex plate body (b1 up to 7.2 mm) provides structural rigidity, reducing deflection and vibration under deep, continuous ripping loads.
- Thin kerf (4.1–5.9 mm) against a reinforced body delivers maximum material yield per log without sacrificing stability.
- Carbide rakers prevent the steel plate sides from contacting the cut wood face, eliminating scoring, plate heat build-up, and lateral friction wear.
- High bending strength and carbide hardness maintain edge integrity through extended wet-wood production runs.
Problems This Saw Blade Helps Solve
- Blade deflection and strip width variation caused by lateral forces in deep, continuous ripping passes.
- Steel plate contact with the wood face, leading to surface scoring, lateral heat, and premature plate wear.
- Chip packing in the kerf on wet-wood sawmill lines, causing binding and feed resistance.
- Short blade life from carbide edges not designed for the combined abrasion of wet fiber and resin in softwood ripping.
Application Notes
- Match diameter, kerf width, body thickness, and side clearance consistently across all blades in the arbor set.
- Maintain chip extraction capacity to prevent chip packing, particularly on wet softwood at high feed rates.
- Regrind on schedule — do not run to heavy wear, as deflection and surface quality deteriorate before edge failure is visible.